Resources / Aluminum Die Casting Wall Thickness Rules

Aluminum Die Casting Wall Thickness Rules

Typical wall thickness ranges, transitions, ribs and bosses for aluminum die casting, and how wall design affects filling, porosity and cycle time.

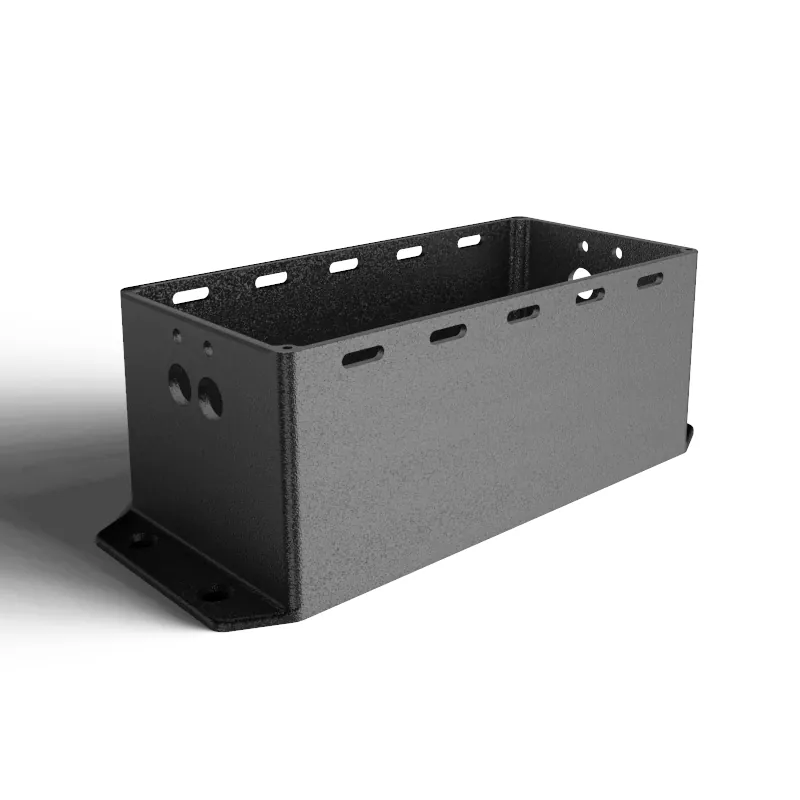
Aluminum wall thickness review Aluminum wall thickness review
Audience
Buyers and engineers
Focus
Practical decisions
Next
DFM review
Output
Actionable checklist
01 / Guide

Why wall thickness drives casting quality

Wall thickness controls how metal fills the cavity, how fast the part solidifies and where shrinkage porosity can form. A wall that is too thin may not fill before the metal freezes; a wall that is too thick holds heat and cools unevenly.

In production the effect is visible in cycle time, scrap rate and the machining cost needed to hold critical features. Wall design is therefore a commercial decision as much as a geometry decision.

  • Thin walls need higher filling pressure and better venting
  • Thick sections cool slowly and can pull shrinkage porosity
  • Uneven walls create hot spots and distortion
  • Wall design changes usually require a tooling change
02 / Guide

Typical wall thickness ranges

For aluminum die casting, general housings and covers commonly use walls between 1.5 mm and 3.0 mm. Small parts with short flow lengths can use thinner walls when the gate, venting and process window are planned for it.

Structural parts and load-bearing housings often sit between 2.5 mm and 4.0 mm. The number should always be confirmed against the flow length, alloy and functional requirement rather than copied from a table.

  • 1.5–2.0 mm: small covers and electronic housings
  • 2.0–3.0 mm: general housings and enclosures
  • 2.5–4.0 mm: structural brackets and load paths
  • Confirm the value against flow length and alloy
03 / Guide

Designing transitions, ribs and bosses

Abrupt thickness changes create hot spots. Use gradual transitions with generous radii so metal can flow and the part can cool at a similar rate across the section.

Ribs should normally be thinner than the main wall, often around 50–70% of wall thickness, with a radius at the base. Bosses should be supported by ribs or a local pad rather than standing as isolated thick sections.

  • Add radii at internal and external corners
  • Keep ribs at about 50–70% of wall thickness
  • Support bosses with ribs or a pad
  • Avoid isolated thick sections
04 / Guide

Machining allowance and datum planning

Where a face will be machined, add enough stock to remove casting skin and any local distortion. A common starting range is 0.3–0.8 mm on machined surfaces, confirmed against the drawing and process capability.

Machining stock should be planned together with the datum strategy, because the casting datum and the machining datum decide whether bores, faces and sealing surfaces stay aligned in production.

  • Plan 0.3–0.8 mm stock on machined faces
  • Define the casting datum before tooling
  • Keep critical features on the same datum chain
  • Confirm the values during DFM review
Buyer questions

Questions to resolve before production.

These answers define the normal project path and the information needed for a useful quotation.

Provide the controlled 2D/3D drawing, material requirement, annual quantity, finishing requirement, critical dimensions, target market and delivery date.

An initial feasibility discussion is possible, but the quotation and tooling scope should be based on a controlled drawing revision.

Tolerance and inspection requirements are defined from the drawing, critical features, process capability and agreed datum strategy.

Ownership, storage, maintenance and transfer terms are defined in the quotation or supply agreement before the tooling project starts.

Related pages

Continue through the project path.

Use the internal links to connect the material, process, industry, product and RFQ pages around one project decision.

Send the drawing. Get the engineering questions first.

Include the material, annual quantity, finishing requirement, target market and delivery date. The review can start from STEP, IGS, DWG, DXF, PDF or ZIP files.

Start an RFQ
Upload drawing