Drawing review
Review the controlled 3D model, 2D drawing, critical dimensions, annual volume and finish requirements.
A production route for thin-wall, dimensionally stable parts where cycle time, tooling design and process control must be planned together.
 High-Pressure Die Casting project review
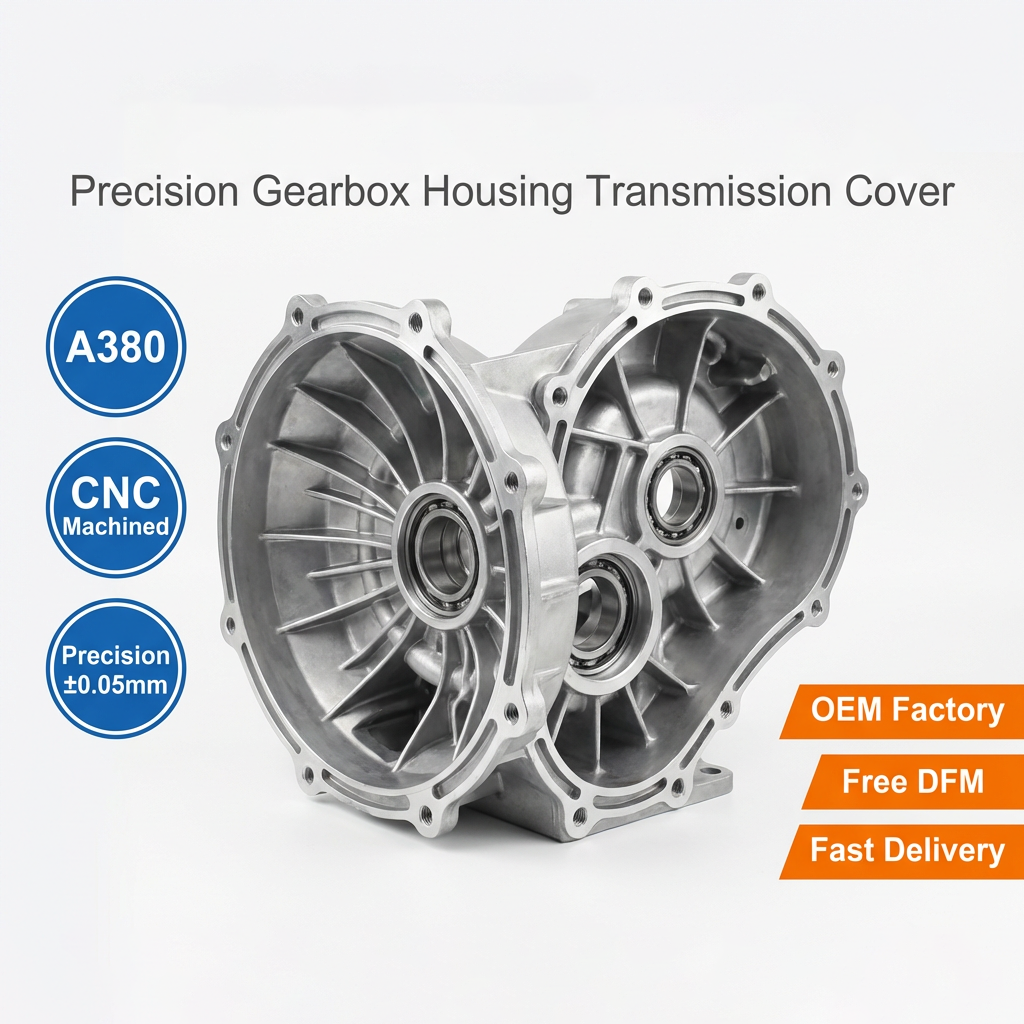
High-pressure die casting injects molten metal into a hardened steel die at high speed and pressure. It is commonly selected for aluminum, zinc and magnesium components that need good surface detail, stable dimensions and efficient volume production.
The process is most effective when the part geometry, gate position, cooling layout, venting, ejection and machining strategy are reviewed as one manufacturing system.
Use this table for project planning, then confirm every critical value against the approved drawing and process plan.
| Core process | Cold-chamber high-pressure die casting |
|---|---|
| Machine range | 160T to 800T across 20+ die casting machines |
| Part weight range | 5 g to 15 kg |
| Materials | Aluminum, zinc and magnesium alloys |
| Tooling | Custom die design and manufacture |
| Secondary operations | CNC machining, finishing, assembly and inspection |
| Tolerance | ±0.05 mm as cast; ±0.01 mm on machined features |
| Lead time | Mold 15-25 days; T1 sample 3-5 days; production 7-15 days |
Each stage produces a decision or document that the next stage depends on. This keeps engineering, purchasing and production aligned.
Review the controlled 3D model, 2D drawing, critical dimensions, annual volume and finish requirements.
Assess wall thickness, draft, ribs, fillets, parting line, gating, venting and porosity risk.
Build the die, run the trial, inspect the sample and define corrections before production approval.
Run the approved process, complete secondary operations and release parts against the inspection plan.
These answers define the normal project path and the information needed for a useful quotation.
Provide the controlled 2D/3D drawing, material requirement, annual quantity, finishing requirement, critical dimensions, target market and delivery date.
An initial feasibility discussion is possible, but the quotation and tooling scope should be based on a controlled drawing revision.
Tolerance and inspection requirements are defined from the drawing, critical features, process capability and agreed datum strategy.
Ownership, storage, maintenance and transfer terms are defined in the quotation or supply agreement before the tooling project starts.
Use the internal links to connect the material, process, industry, product and RFQ pages around one project decision.
Include the material, annual quantity, finishing requirement, target market and delivery date. The review can start from STEP, IGS, DWG, DXF, PDF or ZIP files.